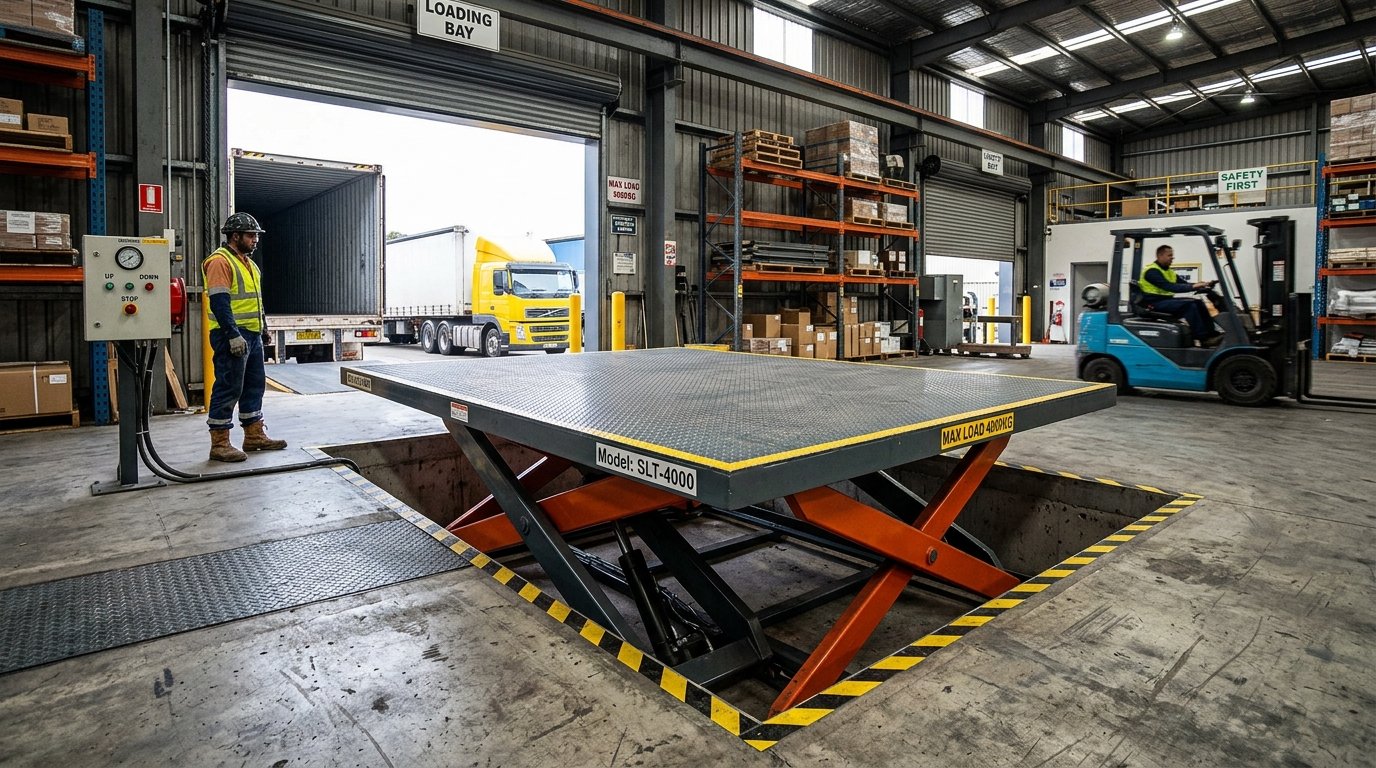
In this technical factory trial, SRE LiftTech safety engineers demonstrate the failsafe capabilities of our high-capacity Dual Mast Hydraulic Goods Lift engineered for a 4-floor manufacturing facility.
### Rigorous Safety Verification Matrix
Our testing protocol subjects the hydraulic power pack and dual synchronized cylinders to extreme operating conditions:
- **Hose Burst Safety Valve (Velocity Fuse):** Immediate automatic lockup preventing platform drop in the event of hydraulic line rupture.
- **Electronic Floor Leveling Sensor:** Micron-accurate sensor calibration ensuring seamless flush dock leveling with heavy forklift traffic.
- **Interlocked Landing Gates:** Bi-directional electro-mechanical door interlocks that prevent elevator motion unless all perimeter gates are latched.
The trial validated a seamless operating cycle under 6,250 kg (125% of rated capacity) with zero pressure drop or structural deflection.
Key Takeaways & Technical Highlights
- 5,000 kg rated capacity with 125% proof load testing verified
- Velocity fuse instantly freezes elevator carriage upon abnormal pressure change
- Synchronized hydraulic flow dividers guarantee level platform ascent
- Heavy-duty chequered plate platform withstands continuous forklift transit