Engineered for extreme reliability and high-load material handling in warehouses, industrial plants, and production facilities.
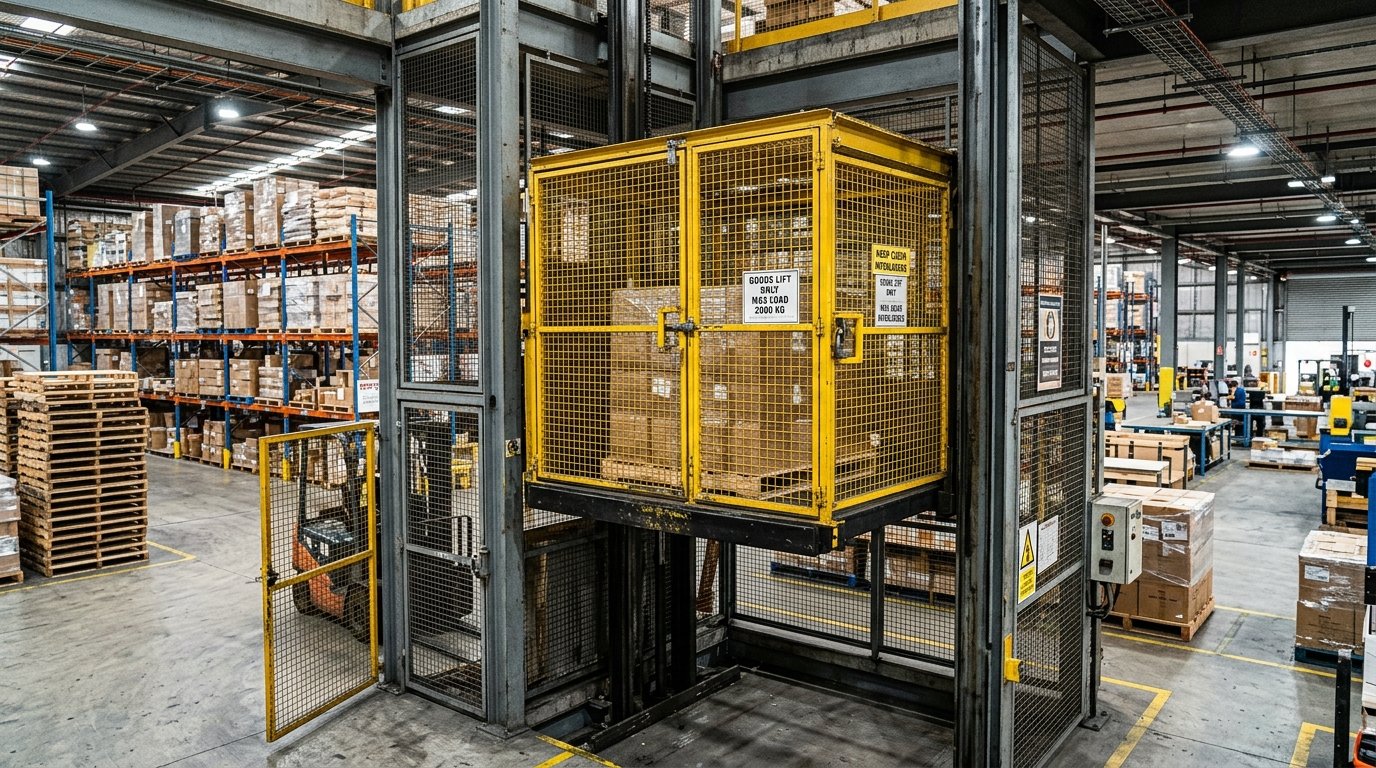
Factory operational and site installation videos for Standard Goods Lift are available on request from our engineering desk.
Mechanical Interlocking Gate System: Dual electrical and mechanical door interlocks prevent elevator operation whenever landing safety gates are open or unlatched.
Emergency Rupture Safety Valve: Hydraulic line burst check valves instantly lock fluid inside the cylinders if any pressure drop occurs, preventing platform drop.
Overload Sensor & Alarm Cut-Off: Electronic pressure load cells detect cage overload and inhibit travel while sounding an audible warning buzzer on all floors.
Multi-Tier Warehouses & Logistics: Fast vertical transport of palletized stock, cartons, and bulk containers across mezzanine levels and multi-tier storage.
Automotive & Heavy Engineering: Lifting heavy automotive parts, engine dies, machinery assemblies, and raw metal sheet bundles between floor levels.
Pharma, Chemical & FMCG Plants: Safe transfer of raw chemical drums, packaging materials, and finished goods in accordance with industrial plant safety standards.
Site Survey & Foundation Prep: Verification of pit depth (or ramp area), overhead clearance, and guide column anchor points against structural RCC walls.
Guide Mast Erection & Cage Assembly: Precision alignment of heavy steel guide channels, hydraulic cylinder mounting, and leaf chain tension calibration.
Power Wiring & Safety Testing: Connecting the 3-phase power pack, configuring floor-limit switches, and performing 125% full load safety drop tests.
A: SRE LIFTECH manufactures heavy-duty Standard Goods Lift units with capacities ranging from 500 kg up to 10 Tons (10,000 kg), designed for rigorous 24/7 industrial factory and warehouse operations.
A: Generally, a shallow concrete pit of 300mm to 500mm is recommended to align the cabin level with the floor. However, we also engineer pit-less models with integrated entry ramps.
A: Every unit includes electrical gate interlocks, emergency fall-arrest safety wedge brakes on guide tracks, hydraulic hose burst lock valves, overload trip alarms, and floor-leveling limit switches.
A: Every SRE LIFTECH goods elevator comes with an authentic 12-month structural and hydraulic warranty, backed by 24/7 engineer support across all major industrial belts in India.
